Industrial Wastewater Treatment Plant in Kuwait: Complete Guide & Technologies by Al Khabeer Water Treatment LLC
We are glad you are here at Al Khabeer Water Treatment LLC, your trusted engineering partner for water and waste water treatment solutions in the region. We design, build, install and maintain custom treatment plants to help factories manage waste water effectively and comply with stringent environmental laws.
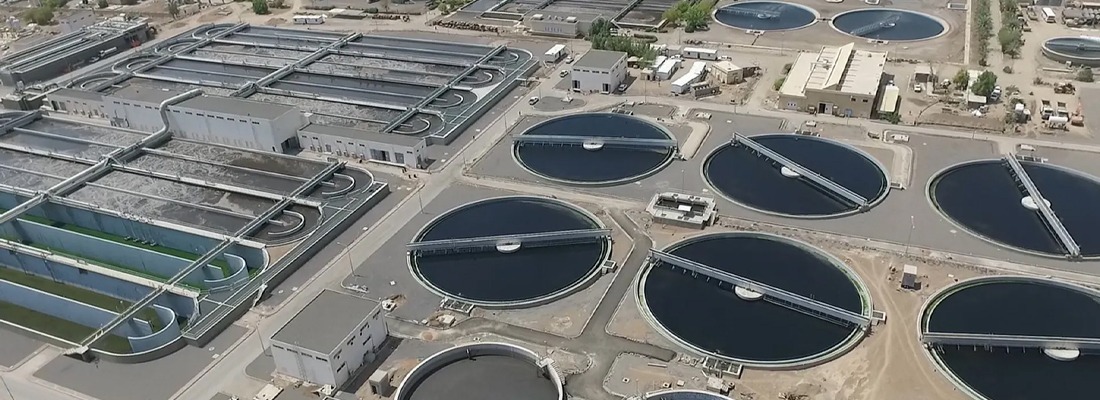
An INDUSTRIAL WASTEWATER TREATMENT PLANT IN KUWAIT allows the factories to deal with complex industrial waste, dispose of toxic chemicals, and recycle clean water in their daily work. We build scalable, energy-efficient units for oil refineries, chemical plants, food manufacturing hubs and commercial centers. Our engineering team designs units for the specific needs of each.
But with water protection becoming a top priority for businesses, they need strong infrastructure to keep natural resources safe and maintain long-term productivity.” We offer a full range of support, from initial site visits and laboratory water analysis to full plant commissioning and 24/7 maintenance agreements.
Business Highlights of Al Khabeer Water Treatment LLC
- Turnkey Engineering: Full design, fabrication, assembly, and commissioning of custom water treatment infrastructure.
- Advanced Technologies: Integration of reverse osmosis, membrane bioreactors, ultrafiltration, and zero liquid discharge systems.
- Specialized Systems: Heavy-duty oil-water separators, automatic pH neutralizers, vacuum evaporators, and vehicle wash recycling.
- Comprehensive Support: 24/7 technical assistance, specialty chemical supply, and long-term operation contracts.
Facility Capabilities & System Solutions
| Operational Feature | System Capability & Technical Focus |
|---|---|
| Effluent Pre-Treatment | Screening, chemical dosing, oil interception, and dissolved air flotation for heavy solids removal. |
| Membrane Separation | Advanced ultrafiltration and reverse osmosis trains to eliminate dissolved impurities and salts. |
| Sludge Dewatering | Mechanical screw presses and polymer dosing units to reduce waste volume efficiently. |
| Water Recycling | High-recovery treatment setups that convert industrial effluent into reusable process water. |
Implementing a modern INDUSTRIAL WASTEWATER TREATMENT PLANT IN KUWAIT ensures that manufacturing plants operate smoothly without risking regulatory fines or workflow disruptions. Our automated control systems provide continuous monitoring, giving facility operators complete peace of mind and operational stability.
Key Treatment Technologies for Industrial Facilities
Reverse Osmosis & Membrane Systems
- High Salt Rejection: Semi-permeable membrane filtration removes up to 99% of dissolved minerals, heavy metals, and trace compounds.
- Process Water Production: Converts brackish industrial discharge into high-quality water suitable for cooling towers and boilers.
- Energy Recovery: Modern membrane layouts reduce overall power consumption during high-pressure filtration cycles.
Membrane Bioreactor (MBR) & Biological Treatment
- Compact Footprint: Combines traditional activated sludge processes with advanced membrane filtration in a space-saving layout.
- High Organic Removal: Efficiently degrades complex organic pollutants, reducing biochemical and chemical oxygen demand.
- Consistent Permeate: Delivers clear, silt-free water ready for advanced polishing or direct non-potable reuse.
Vacuum Evaporation & Zero Liquid Discharge (ZLD)
- Maximum Water Recovery: Concentrates heavy liquid waste to separate clean distilled water from concentrated solids.
- Zero Effluent Release: Eliminates liquid discharge entirely, enabling compliance with strict environmental regulations.
- Waste Reduction: Reduces total liquid waste volume significantly, lowering overall disposal handling needs.
Using a custom-built INDUSTRIAL WASTEWATER TREATMENT PLANT IN KUWAIT equips industrial operations to extract maximum value from every gallon of water used. By combining physical clarification with membrane purification, our clients achieve exceptional water clarity while upholding high safety standards.
Industrial Applications & Sector Solutions
Oil, Gas & Petrochemical Refineries
- Removes emulsified oils, sulfides, phenols, and hydrocarbons from heavy refinery wastewater.
- Utilizes specialized oil skimmers and dissolved air flotation units prior to biological polishing.
- Recycles treated water for utility services, fire systems, and reservoir pressure maintenance.
Manufacturing & Heavy Chemical Industry
- Neutralizes acidic or alkaline discharges using automated pH balancing systems.
- Extracts heavy metal traces, pigments, and synthetic chemical compounds safely.
- Prepares process water for closed-loop manufacturing and equipment cooling lines.
Food, Beverage & Commercial Processing
- Handles high organic loads, fats, oils, grease, and suspended organic matter effectively.
- Incorporates odor control units and hygienic biological filtration systems.
- Provides recycled water systems for vehicle washing and facility sanitation.
Sector-Specific Treatment Focus
| Industrial Sector | Primary Treatment Strategy |
|---|---|
| Petrochemical & Energy | Dissolved air flotation, oil-water separation, and advanced oxidation filtration. |
| Chemical Manufacturing | Automatic pH neutralization , chemical precipitation, and reverse osmosis polishing. |
| Food & Beverage | Biological treatment, grease traps, and ultrafiltration for organic matter removal. |
| Automotive & Services | Compact oil interceptors, vehicle wash recycling, and multimedia filtration. |
Choosing an experienced partner like Al Khabeer Water Treatment LLC guarantees an INDUSTRIAL WASTEWATER TREATMENT PLANT IN KUWAIT engineered specifically for your facility's unique effluent profile. Our sustainable systems allow businesses to lower water footprint demands, protect surrounding ecosystems, and achieve long-term economic growth.
Frequently Asked Questions (FAQs)
Why MODERN FACTORIES NEED AN INDUSTRIAL WASTEWATER TREATMENT PLANT KUWAIT?
It removes harmful physical, chemical and biological contaminants from factory effluent before it is released. This guaranties full environmental compliance, protects local ecosystems and provides clean recycled water for internal factory processes.”
How to Improve the Efficiency of Wastewater Recycling Using Reverse Osmosis Technology?
Reverse osmosis uses high pressure membrane separation to filter out dissolved salts, heavy metals and microscopic impurities. The process generates high-purity water which may be reused in cooling towers, boilers and industrial wash systems.
What are the key advantages of Zero Liquid Discharge (ZLD) systems?
Zero Liquid Discharge systems process and recycle all liquid waste stream and leave only dry solid waste. This eliminates all environmental liquid discharges, minimizes raw water usage and solves hard waste management problems.
Is it possible to recycle treated industrial effluent within the plant?
Yes, industrial effluent properly treated is of very stringent quality standards for non-potable use. This reclaimed water is safely used by facilities to flush utilities, cool equipment, suppress dust and irrigate landscapes.
How does Al Khabeer Water Treatment LLC help in the long term operation of plants?
We provide full end-to-end support including custom engineering design, equipment supply, professional installation and 24/7 maintenance services. Our technical teams maintain the operation of the plants, the flow of chemicals and the integrity of compliance.

